Stud Welding with Tip Ignition
Capacitor-discharge stud welding with tip ignition is used to weld primarily pin-shaped metal parts with diameters ranging from approximately 1 to 10 mm onto mostly thin sheet metal ranging from 0.5 to approximately 3 mm in thickness. It is divided into two methods: contact welding and gap welding.
The Difference
The gap method differs from the contact method in that, after the trigger is pulled, the bolt is lifted by a lifting magnet in the gun to a preset stroke or gap and is then accelerated toward the workpiece by spring force.
Contact Welding
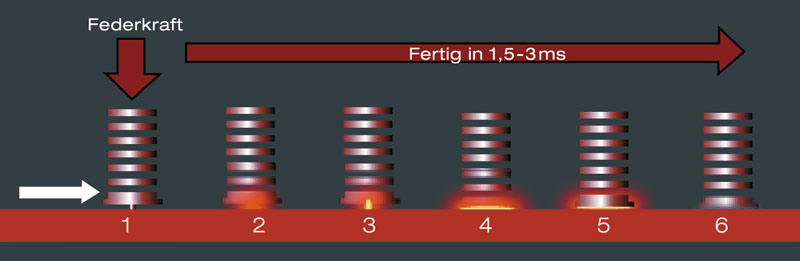
The contact method is preferred for stainless steel as well as unalloyed and zinc-coated sheets (–15 µ). In this process, the welding stud is inserted into the stud holder and placed against the workpiece surface using a hand-held gun or an automatic welding head. A compression spring inside the welding gun presses the stud—with its ignition tip, which is characteristic of capacitor stud welding—against the workpiece. When the trigger button on the welding gun is pressed, the energy stored in the capacitors is released via a thyristor. The stud’s ignition tip heats up so intensely that it melts instantly and partially vaporizes. The resulting arc completely fuses the stud end to the workpiece. After a welding time of just 1–3 ms and a welding current of up to 15,000 A, the stud and base material are homogeneously joined, with a very narrow melt zone of only a few tenths of a millimeter. This allows bolts to be welded to very thin sheets of metal without any unsightly marks or discoloration being visible on the reverse side.
The Splitting Process
The gap method differs from the contact method in that, after the trigger is pulled, a lifting magnet in the gun raises the bolt to a preset stroke or gap and then accelerates it toward the workpiece using spring force. As soon as the spark tip of the bolt touches the workpiece, the arc ignites. By adjusting the gap, the arc duration or welding time can be varied; however, it is generally shorter than with the contact method. For this reason, the gap method is preferred for materials with a low melting point, such as aluminum or brass. The welding time is a maximum of 1.5 ms, and the molten zone is even smaller than with the contact method. However, it is even more important to ensure that the workpiece surface is clean and free of electroplated coatings, oil, rust, or scale.

Stud Welding with Short-Stroke Ignition
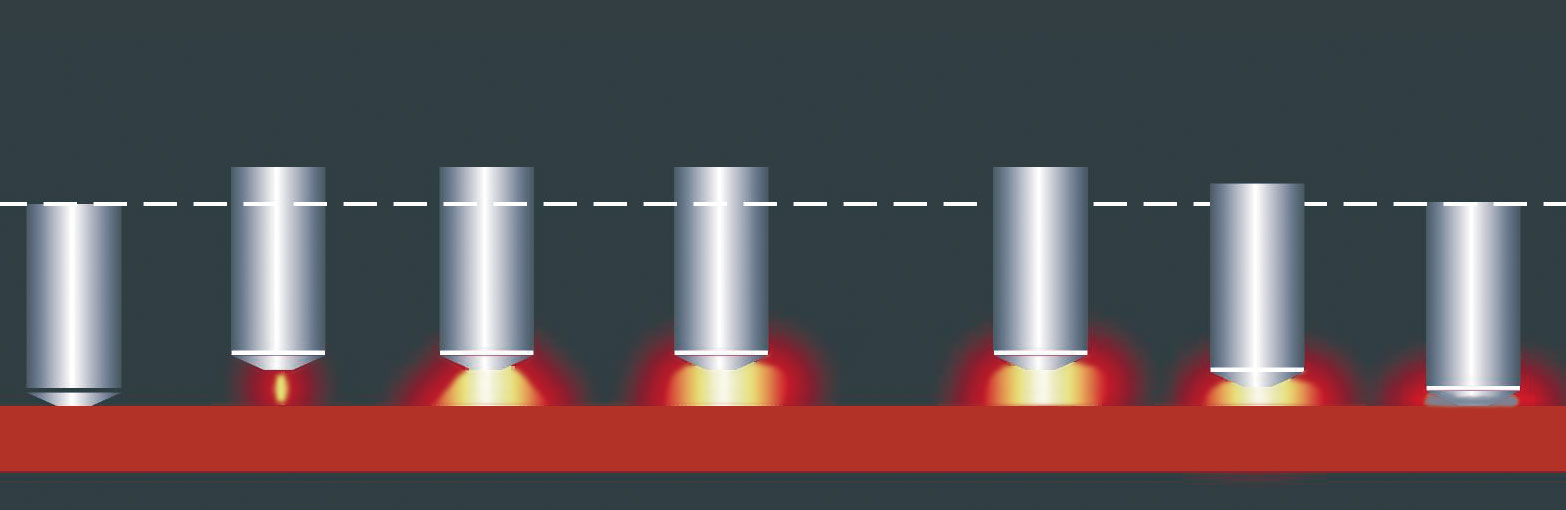
Strike-ignition arc stud welding is used to weld primarily pin-shaped metal parts with diameters ranging from 3 to 30 mm onto metal workpieces with a thickness of 0.8 mm or greater. A distinction is made between two processes: short-cycle spark welding and spark welding with a ceramic ring or shielding gas. The short-stroke ignition process is primarily used for welding flange studs with diameters ranging from 4 to 10 mm onto thin sheets, including those with electroplated coatings thinner than 30 µ. The main area of application is the automotive industry, with up to 600 studs per body-in-white. In this process, the stud is inserted into the stud holder of the welding gun or the automatic welding head, and the gun is supported on the workpiece using a positioning tube, support foot, or gas attachment. After pressing the trigger on the gun, a lifting magnet inside the gun lifts the stud off the workpiece, and a pilot arc is ignited. The main current is then switched on via a transformer and a thyristor bridge. The arc completely melts the stud end and the workpiece surface, and once the preset welding time has elapsed, the lifting magnet releases and a spring pushes the stud into the molten weld pool. After a welding time of 5–100 ms and 500–1,500 A, depending on the application and stud diameter, the stud and base material are homogeneously joined and exhibit a narrow fusion zone of approximately 1/8 of the stud’s diameter. Unlike capacitor discharge welding, this process does not produce a loud bang, and process reliability is higher due to the welding time being approximately 10 times longer.
The Plus
This process can be enhanced with shielding gas; specifically, the shielding gas replaces the ceramic ring, which significantly reduces porosity in the molten metal and produces a neater, fillet-shaped weld bead. A mixed gas consisting of 82% argon and 18% CO₂ is used as the shielding gas, which is supplied via a suitable shielding gas attachment on the welding gun. With welding times ranging from 5 to 300 ms and currents from 500 to 1,500 A, studs with diameters of 3 to 12 mm can be welded onto clean sheet metal with a thickness of at least 1/8 of the stud’s diameter. Aluminum materials can only be processed to a limited extent using arc ignition.
Stud Welding with DA Striker Ignition
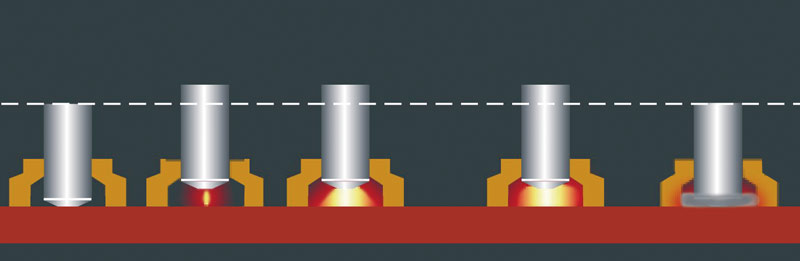
In the ceramic ring arc welding process, a ceramic ring is used as a weld pool shield to shape the molten pool, stabilize the arc, shield the atmosphere, and protect the welder from UV radiation. The ceramic ring is used for a single weld and is removed from the stud by breaking it apart once the molten metal has solidified. An aluminum ball (ignition ball) pressed into the center of the stud’s cone serves as a flux and acts as a deoxidizer. This process is most commonly used in steel and mechanical engineering, where threaded bolts or studs with diameters ranging from 6 to 25 mm are welded to thick steel plates or beams larger than 1/4 of the bolt diameter, with welding times of 100–1,000 ms and 800–2,600 A.
The Plus
This process can be enhanced with shielding gas; specifically, the shielding gas replaces the ceramic ring, which significantly reduces porosity in the molten metal and produces a neater, groove-shaped weld bead. A mixed gas consisting of 82% argon and 18% CO₂ is used as the shielding gas, which is supplied via a suitable shielding gas attachment on the welding gun. With welding times ranging from 5 to 300 ms and currents from 500 to 1,500 A, studs with diameters of 3 to 12 mm can be welded onto clean sheet metal with a thickness of at least 1/8 of the stud’s diameter. Aluminum materials can only be processed to a limited extent using arc ignition.