
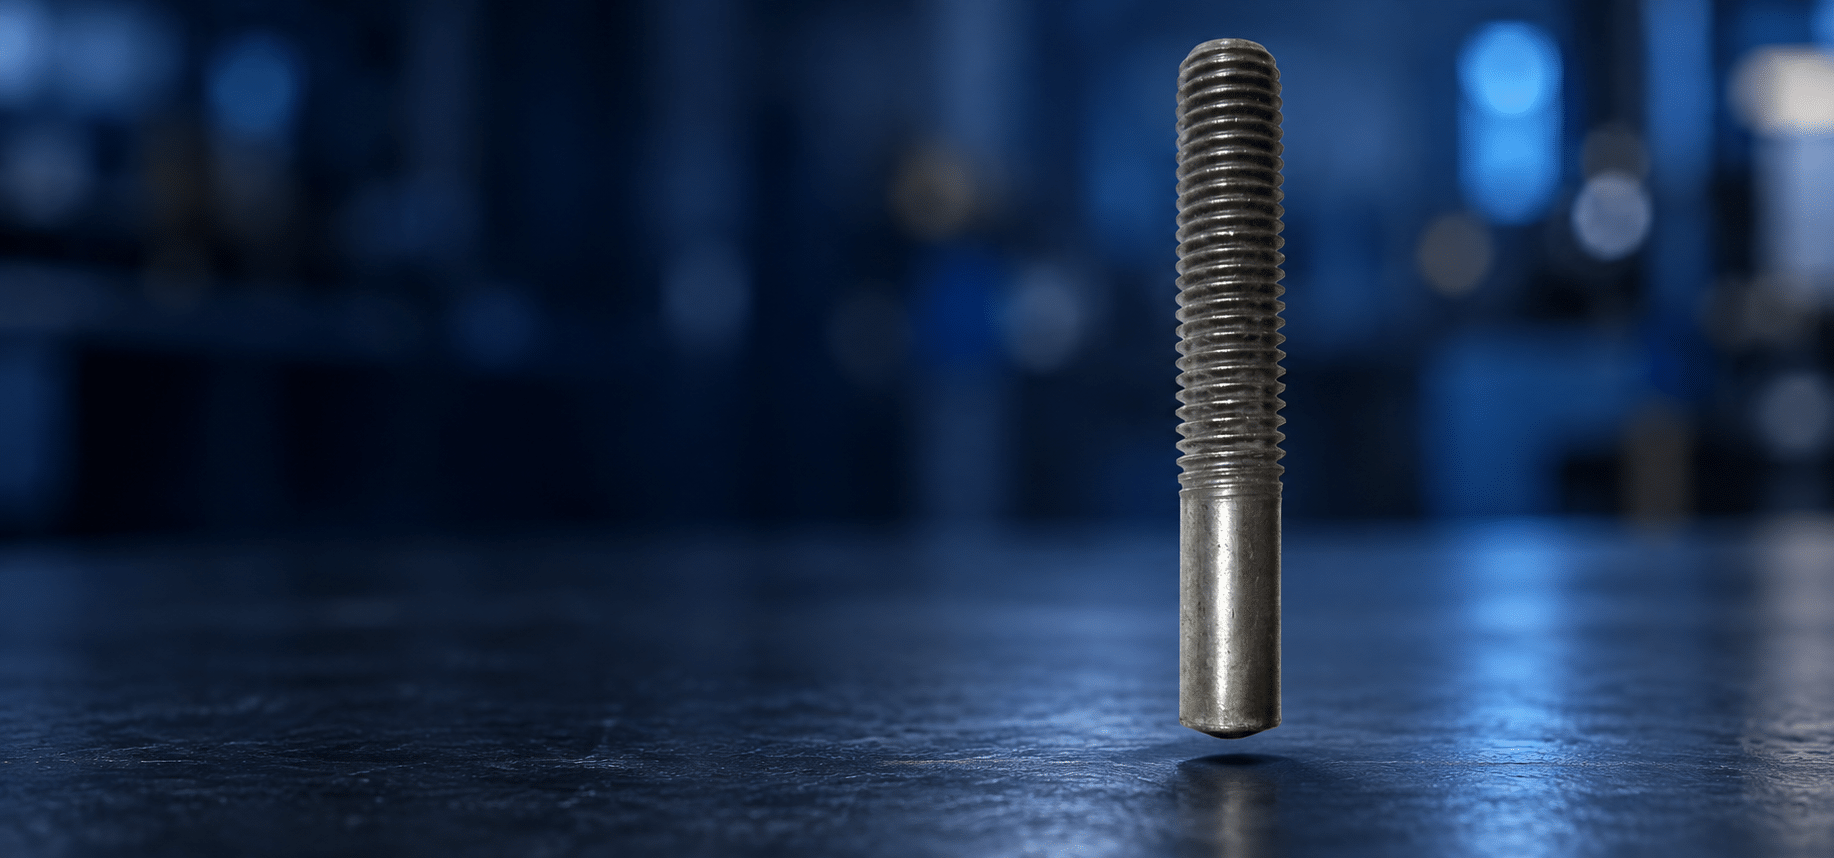
PARTIALLY THREADED STUDS
TYPE PD
PARTIAL THREAD.
SMOOTH SHANK.
| Welding process | Drawn arc welding |
|---|---|
| Thread sizes | M6–M20 |
| Standard reference according to the data sheet | DIN EN ISO 13918:2018 |
| materials | Steel 4.8 without copper plating · Stainless steel A2-50 |
| Ceramic ferrule | PF (product designation); select to suit stud diameter and supplied version |
| Shielding gas | Without aluminium flux up to M12 |
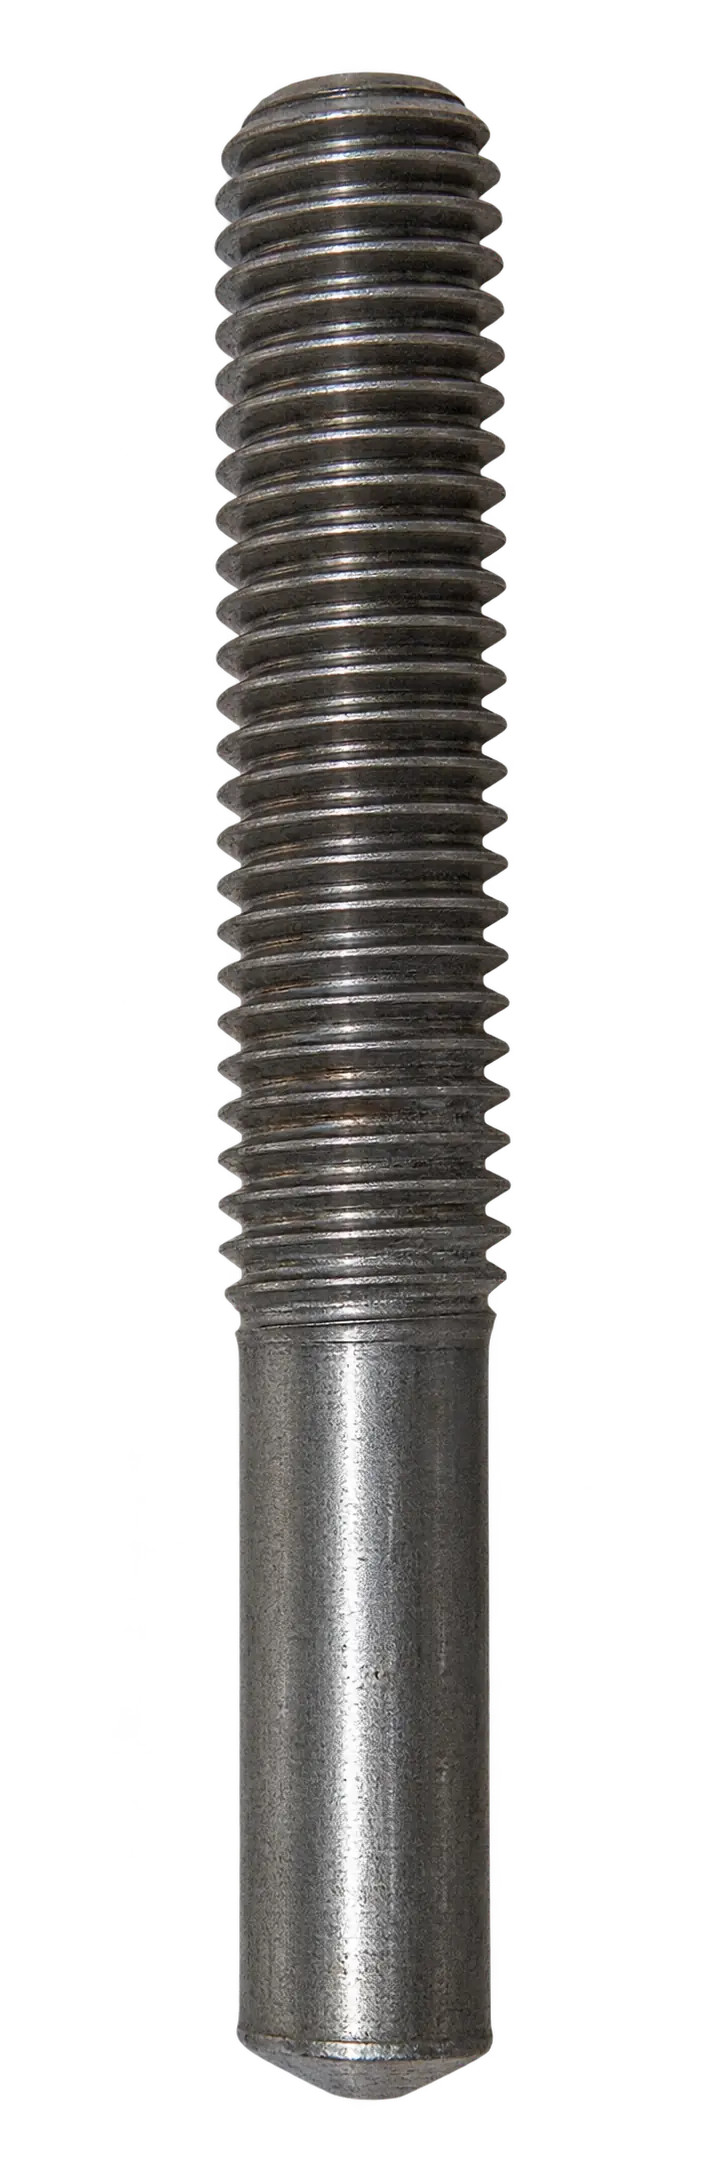
Type PD partially threaded studs: shape and version
PD: dimensions
and materials

| d₁ | d₂ | d₃ | h₄ | y min |
|---|---|---|---|---|
| M6 | 5,30 | 8,50 | 3,50 | 9 |
| M8 | 7,10 | 10,00 | 3,50 | 9 |
| M10 | 8,95 | 12,50 | 4,00 | 9,5 |
| M12 | 10,80 | 15,50 | 4,50 | 11,5 |
| M16 | 14,60 | 19,50 | 6,00 | 13,5 |
| M20 | 18,30 | 24,50 | 7,00 | 15,5 |
α = 140° ±7°. The sheet prints l₂ ±0.05 mm; this unusual length tolerance and the formula for b must be confirmed before ordering.
| d₁ | l₂ in mm |
|---|---|
| M6 | 15, 20, 25, 30, 35, 40 |
| M8 | 20, 25, 30, 35, 40, 45, 50 |
| M10 | 20, 25, 30, 35, 40, 45, 50, 60, 70, 100 |
| M12 | 25, 30, 35, 40, 45, 50, 60, 70, 100 |
| M16 | 30, 35, 40, 45, 50, 60, 70, 100 |
| M20 | 40, 45, 50, 60, 70, 100, 150 |
*The overall range of 15–150 mm does not apply to every size. Other lengths by agreement. Blank data sheet fields are not interpreted as available combinations.
| Material | Class | Designation in the sheet | Code |
|---|---|---|---|
| Steel without copper plating | 4.8 | St. 37 | 71-xxx-xxxx |
| Stainless steel | A2-50 | 1.4301 | 72-xxx-xxxx |
Ordering example according to the data sheet: PD M6×15 in 4.8 without aluminium ball → item no. 71-006-4015. Codes: 0 = original material, 1 = zinc-plated surface, 4 = without aluminium ball.
Type PD partially threaded studs
for industrial tasks
Structural steelwork
Vehicle manufacturing

Mechanical engineering

Plant engineering

Rail vehicles
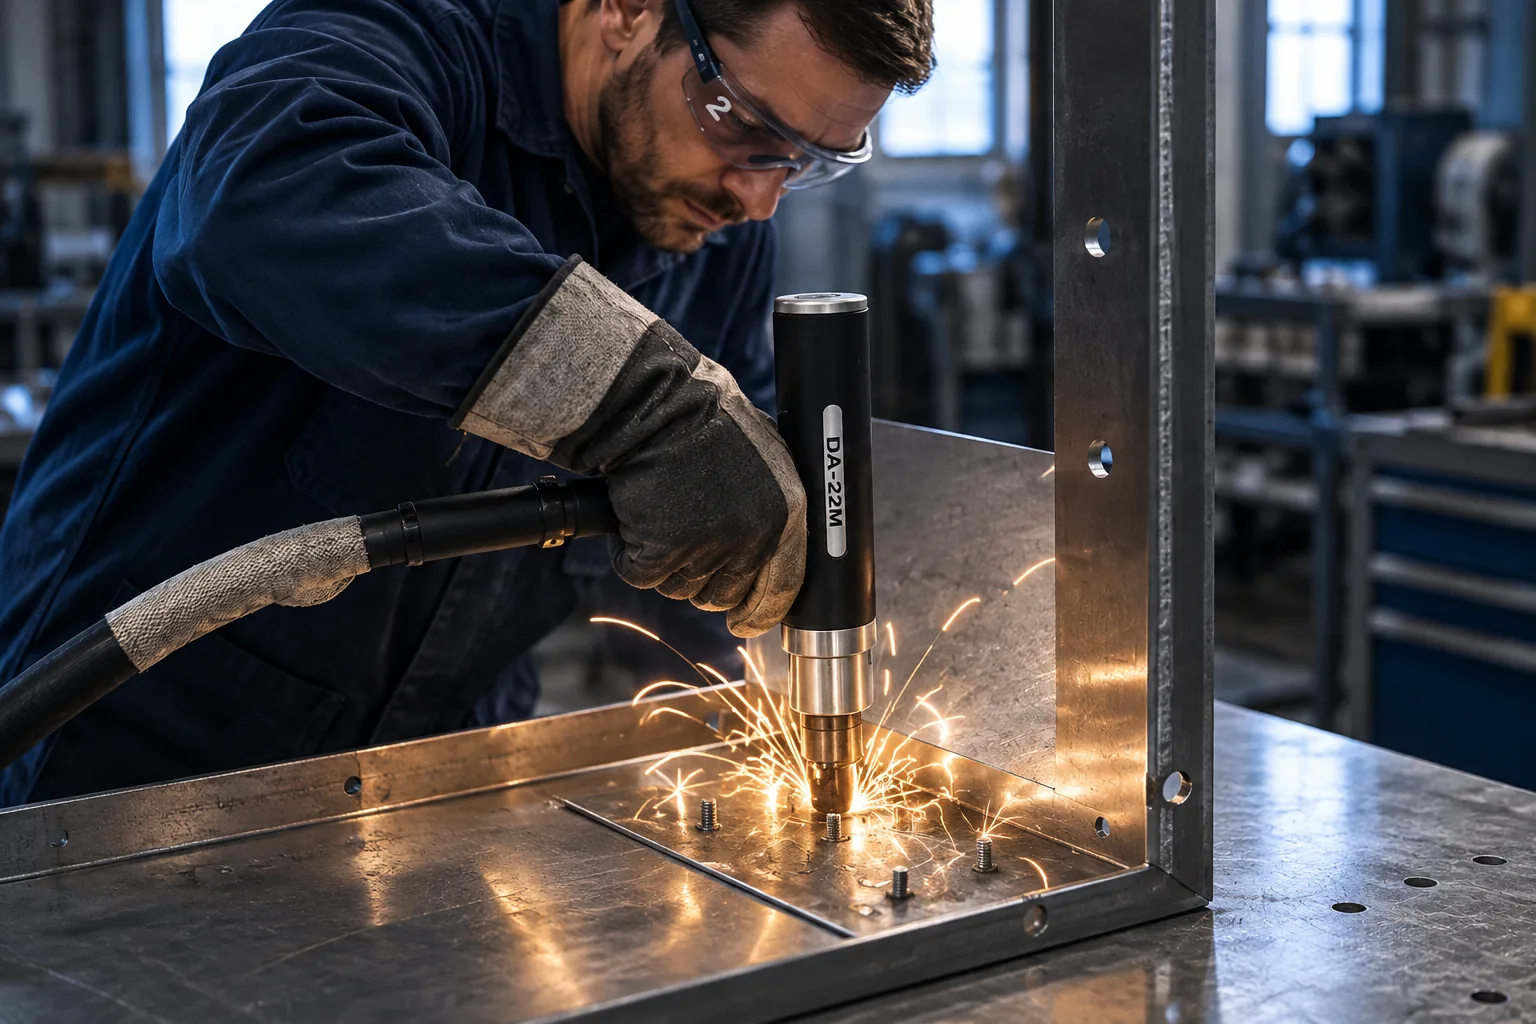
Metal fabrication
Stud welding
with drawn arc welding
Equipment for
PD welding tasks
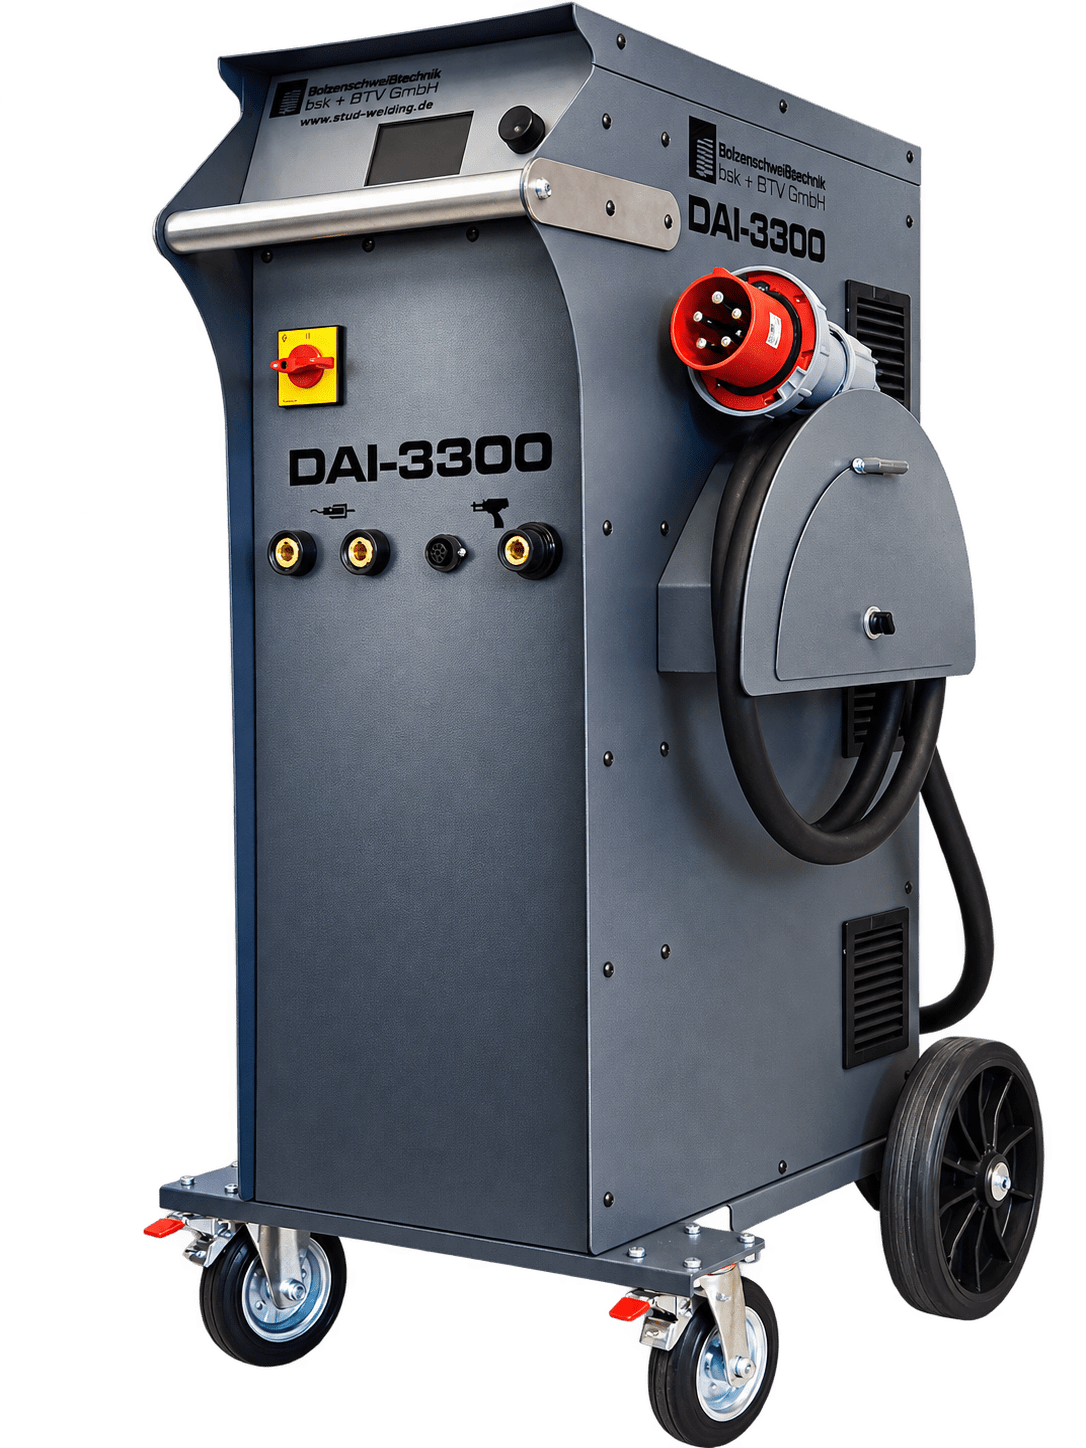
DAI-3300
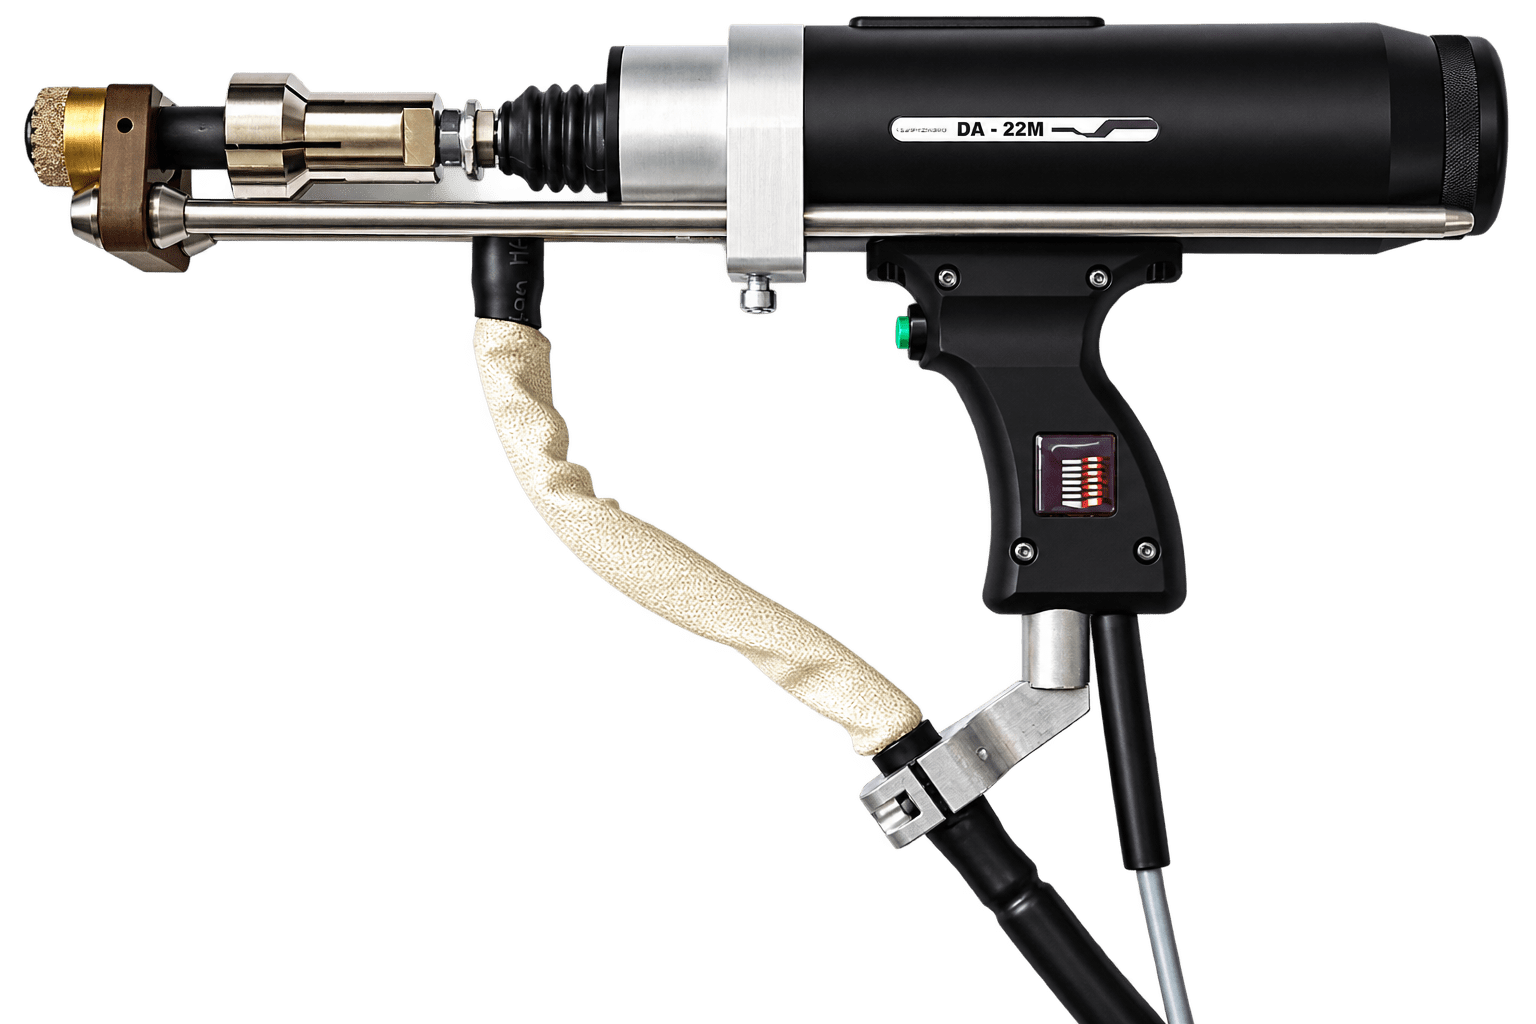
DA-22M

Automation & CNC
Frequently asked questions
about type PD partially threaded studs
Which sizes and lengths are documented?
The data sheet specifies M6–M20 and an overall l₂ range of 15–150 mm. The table shows only combinations with an entry in the manufacturer’s sheet. Other lengths and current availability are clarified on request.
Which materials are offered?
The product page specifies steel 4.8 without copper plating and stainless steel A2-50. Surface finish and ordering codes from the data sheet must be checked against the required variant.
What distinguishes the design?
The supplied original photo shows the partially threaded stud with a clearly defined plain shank. The drawing identifies thread length b, unthreaded section y and shank diameter d₂. The product text and data sheet identify this version as type PD.
Which welding process is used?
Drawn arc welding – manually or fully automatically. With aluminium flux and PF ceramic ferrule for M6–M20; under shielding gas without aluminium flux only up to M12 according to the source.
How do I read the dimensional table?
l₁ denotes the length before welding, l₂ the length afterwards. d₃ and h₄ describe the weld collar area. α = 140° ±7°. The sheet prints l₂ ±0.05 mm; this unusual length tolerance and the formula for b must be confirmed before ordering.
Which ceramic ferrule is used for the product?
The manufacturer specifies type PF. Ferrule and element must be selected to suit the size and application. The specific combination must be confirmed for the required version supplied.
Is every illustrated item of welding equipment suitable for all sizes?
No. The cards show examples of drawn arc welding equipment. A complete approval matrix for all PD sizes and materials is not available. Unit, gun, welding head, holder and weld pool protection are selected for your task.
Are other lengths or special versions possible?
We manufacture special studs to individual requirements. Send the size, required length, material, quantity and, where applicable, a drawing. The specific version is reviewed.

