
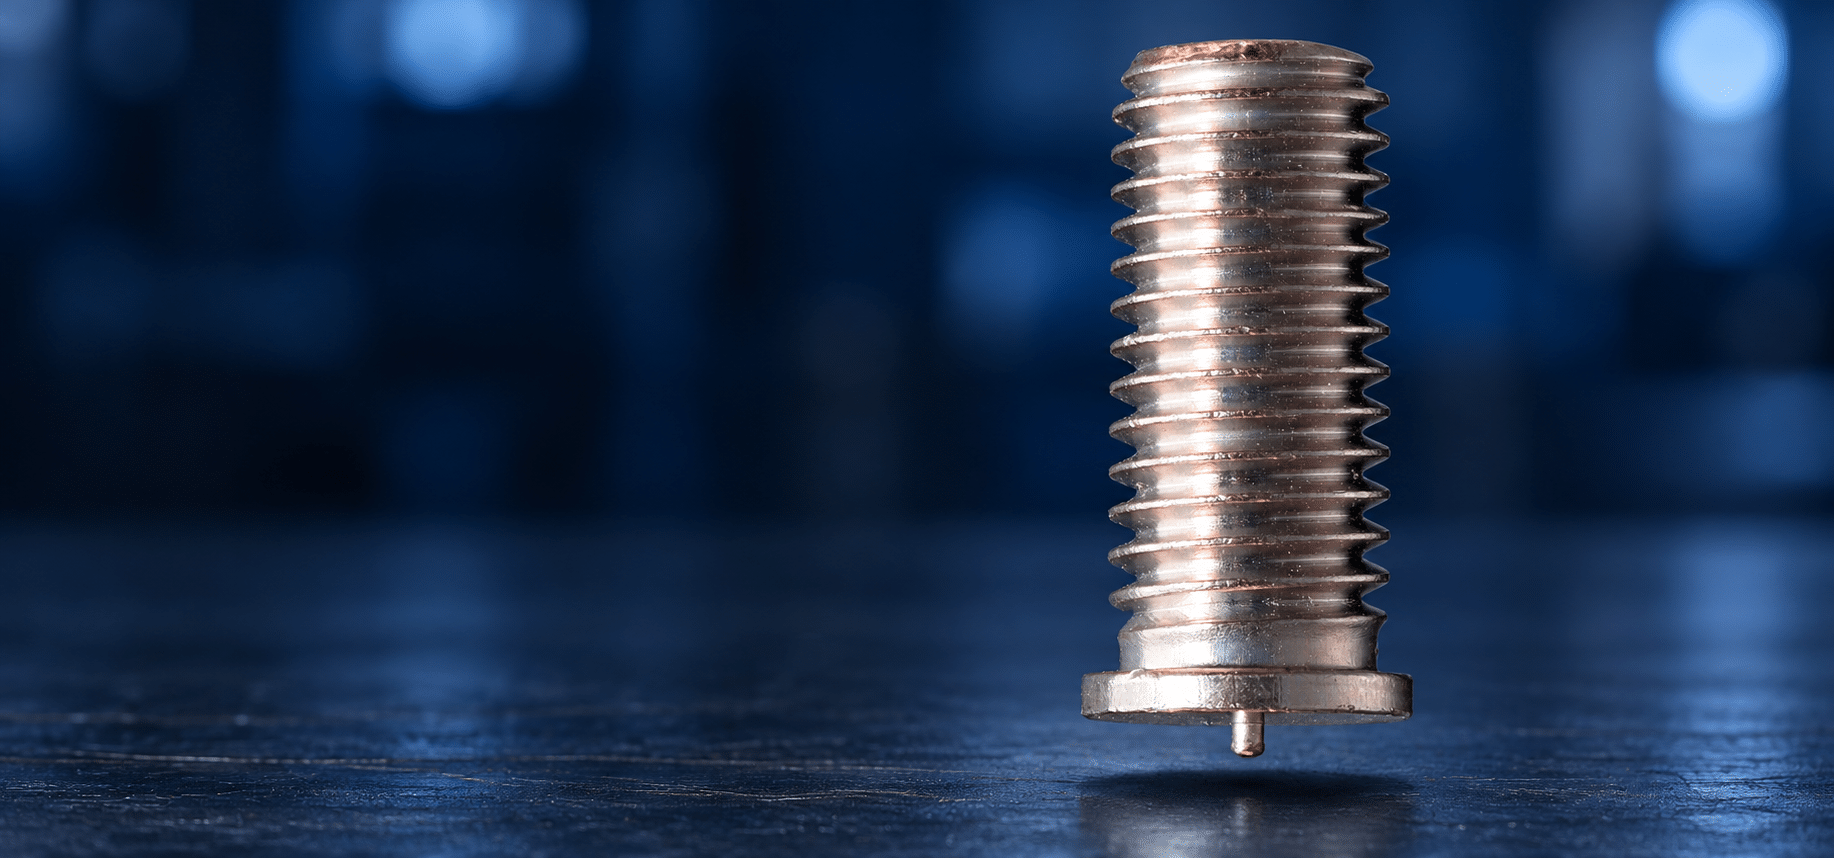
Threaded studs
PT
FLANGE.IGNITION TIP.CAPACITOR DISCHARGE.

| Standard | DIN EN ISO 13918 |
| Welding process | Capacitor discharge (CD) |
| Thread sizes | M3 to M10 |
| Design | Threaded stud with flange and ignition tip |
| Lengths | 6 to 60 mm, depending on thread size |
| Special dimensions | On request |
| materials | Steel 4.8, copper-plated; stainless steel A2-50; aluminium AlMg3 |

PT threaded studs for capacitor discharge welding.
PT threaded studs
in accordance with DIN EN ISO 13918
| Thread d₁ | Flange d₂ ±0.2 | Ignition tip d₄ ±0.08 | Ignition tip l₃ ±0.05 | h₅ max. |
|---|---|---|---|---|
| M3 | 4,5 | 0,60 | 0,55 | 0,6 |
| M4 | 5,5 | 0,65 | 0,55 | 0,6 |
| M5 | 6,5 | 0,75 | 0,80 | 1,0 |
| M6 | 7,5 | 0,75 | 0,80 | 1,0 |
| M8 | 9,0 | 0,75 | 0,85 | 1,5 |
All dimensions in mm. According to the dimensional sheet, the length after welding is approximately l₂ = l₁ − 0.3 mm.
| Steel | 4.8, copper-plated |
|---|---|
| Stainless steel | A2-50 |
| Aluminium | AlMg3 |
Order enquiry
Please specify the thread size, length, material and required quantity, for example: PT M6 × 20 mm, copper-plated steel 4.8.
PT threaded studs have a flange and ignition tip and are processed using capacitor discharge welding. Further dimensions and special designs are available on request.
PT threaded studs
for thin sheets and industrial applications
Control cabinet & enclosure manufacturing
General sheet metal fabrication
Electrical engineering & electronics
Equipment manufacturing
Facade & metal construction
Medical & laboratory technology
Stud welding
with capacitor discharge
Still unsure which stud to choose?
Find the right solution for your application.
START SOLUTION FINDEREquipment for
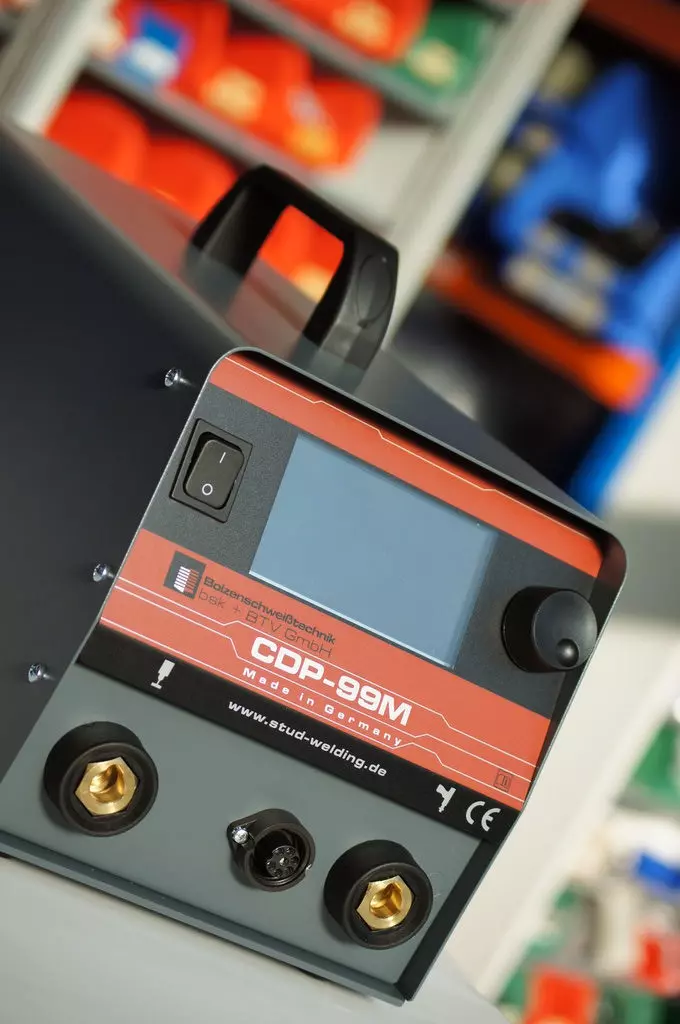
PT threaded studs

Frequently asked questions
about PT threaded studs
Which thread sizes and lengths are available for PT?
The product overview covers M3 to M10 and lengths from 6 to 60 mm, depending on thread size. The linked manufacturer’s dimensional sheet shows M3 to M8. We confirm further dimensions and availability of the required version on request.
Which materials are available?
PT threaded studs are available in copper-plated steel 4.8, stainless steel A2-50 and aluminium AlMg3. We review further materials and special designs on request.
What are the functions of the flange and ignition tip?
The PT has a flange at the welding end and a defined ignition tip. The ignition tip initiates the welding process and melts during it. The flange remains part of the stud.
What changes during welding of the PT stud?
The ignition tip melts and the stud is joined to the workpiece. According to the manufacturer’s dimensional sheet, the length after welding is approximately 0.3 mm shorter. The actual joint geometry depends on the material and welding parameters.
What should be considered when designing the joint?
Stud dimensions, material, sheet thickness and loading must suit the application. Joint suitability must be assessed for the specific welding task using appropriate tests. We support the selection process.
Are ceramic ferrules required for PT?
PT threaded studs are processed using capacitor discharge welding. RF ceramic ferrules are not used for this process. They are used for corresponding drawn arc welding applications.
Which units and welding guns are suitable for PT?
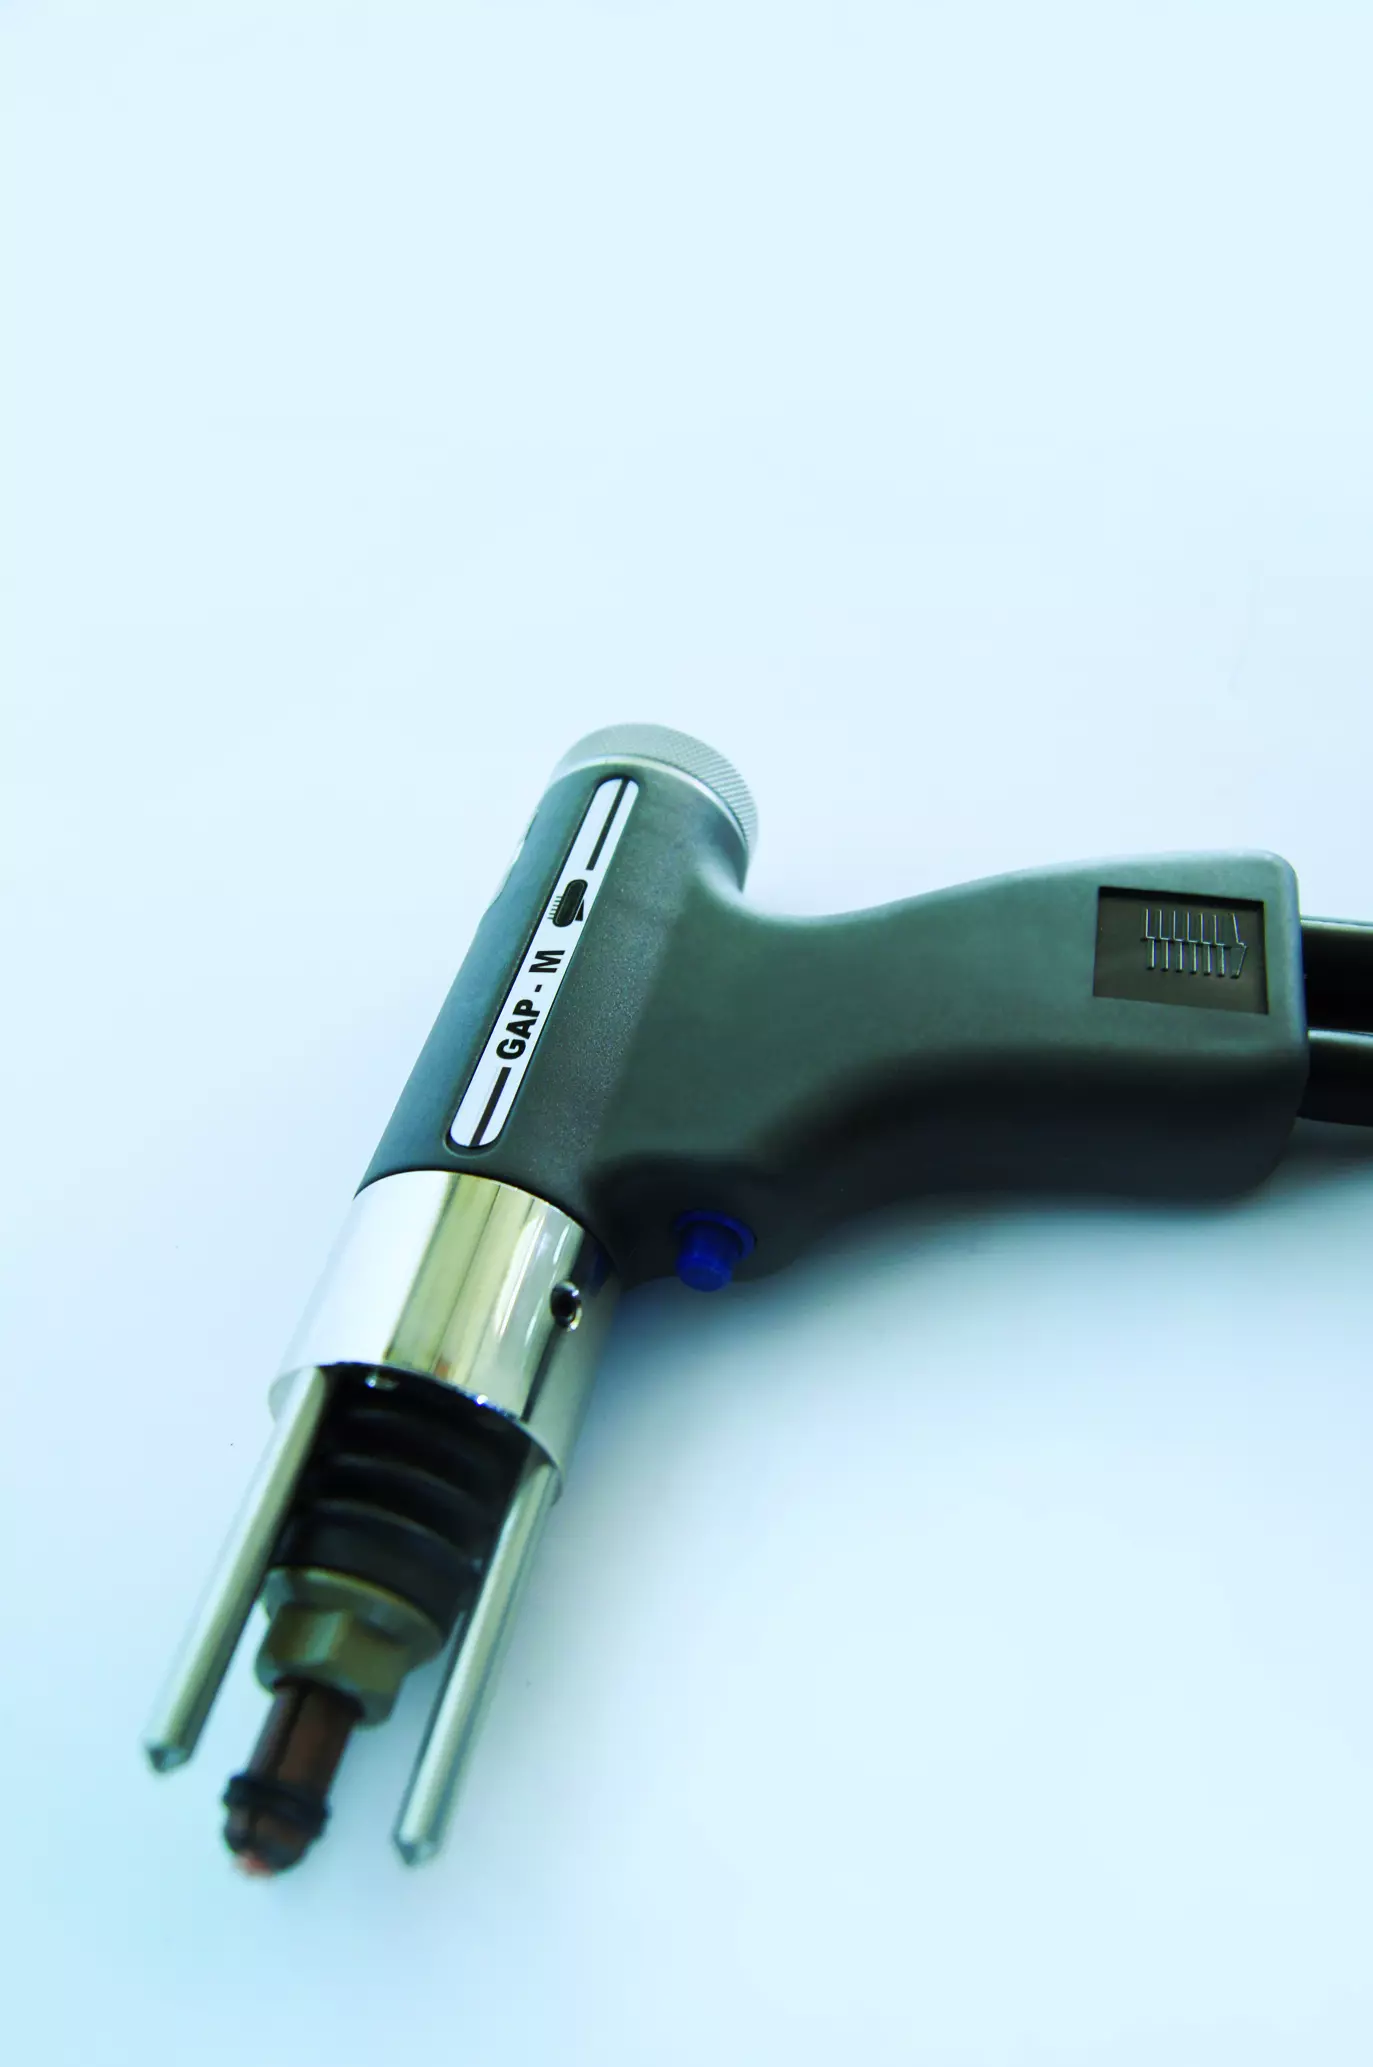
Suitable equipment includes capacitor discharge stud welding units such as CDP-99M with appropriate guns for the contact or gap method. The manufacturer’s page lists GAP-M among others. The combination is selected to suit the material, stud size and welding task.
Are special dimensions available?
Yes. Further dimensions and materials are available on request. We review a suitable version for your application.


