
ATP-8
AI
TECHNICAL DATA
M3–M8
Ø 8 mm
1.50 kg
3 m
25 mm²
1.0–6.0 mm
ATP-8 OR ATP-8M?

Capacitor discharge, short-cycle drawn arc and drawn arc welding
Process-dependent sequence
The following steps describe the basic sequence. Ignition and lift movement differ according to the selected process.
More about stud welding processesPrepare the gun
The gun is set up for the selected welding process. Studs are fed manually or through a suitable automatic feeding system.
Ignite the arc
The appropriate power unit supplies the welding current. The arc melts the stud end and workpiece surface.
Plunge the stud
The stud plunges into the weld pool. The stud and base material solidify to form a joint.
Features
Standard version
Lift adjustment
Plain bearing guide
Thermoplastic housing
Welding current cable
Mechanical design
APPLICATIONS & MATERIALS

 AI-generated · example
 AI-generated · example
ATP-8 and compatible power units
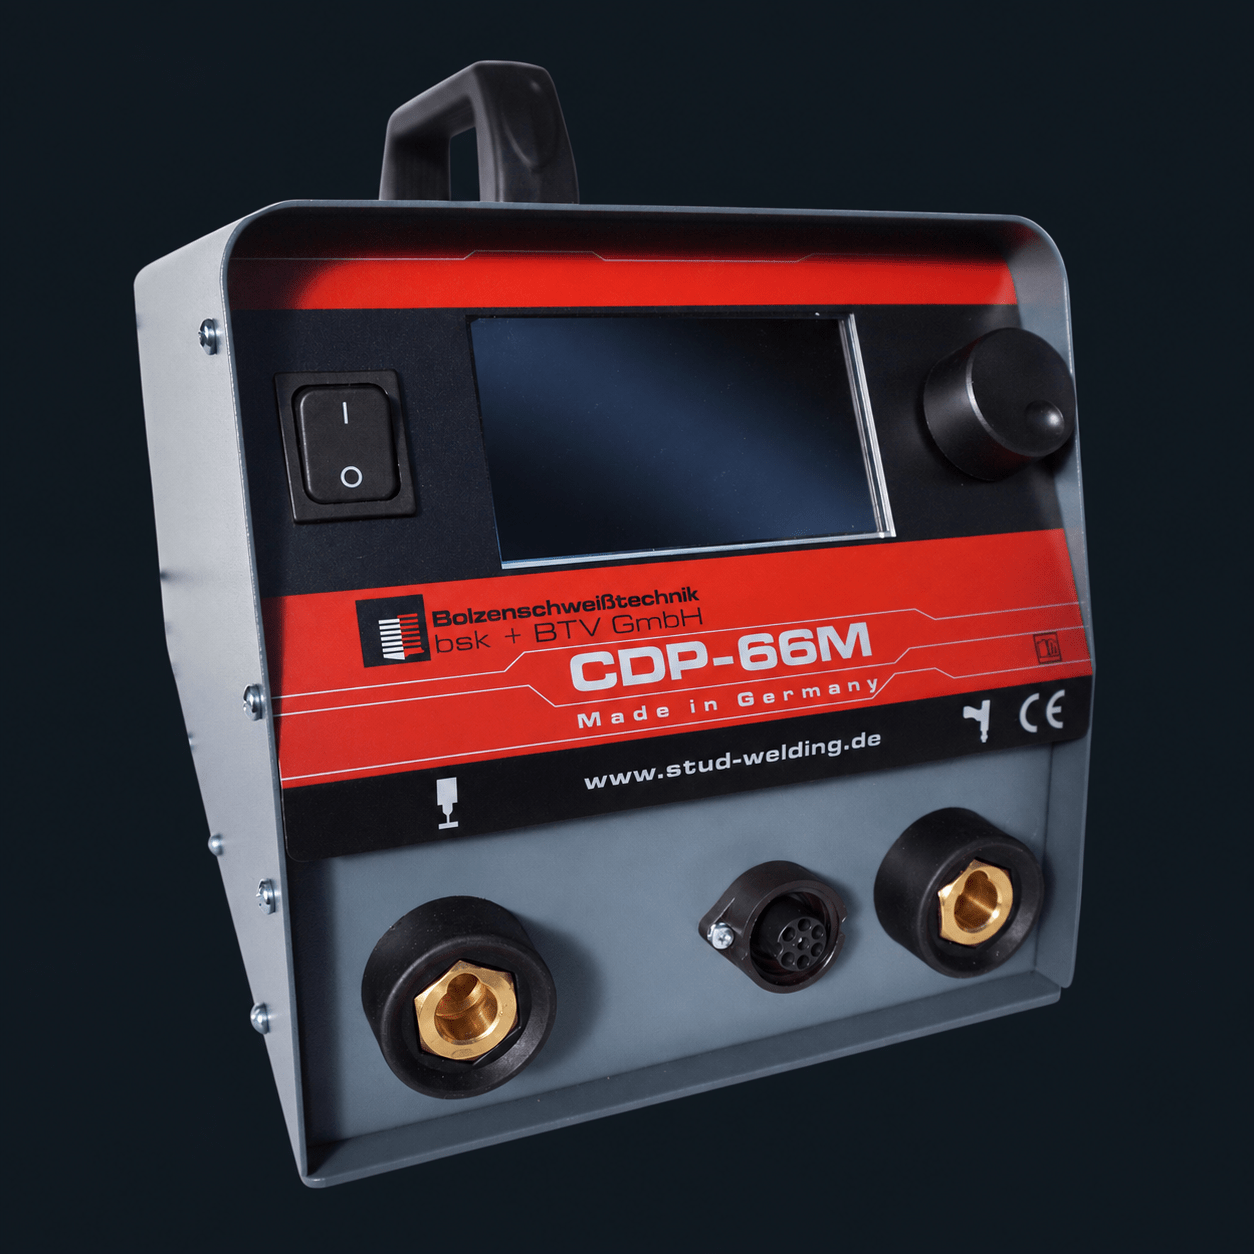
CDP-66M
Compact power unit for capacitor discharge applications and steel or stainless steel studs up to M8.
- Displacement measurement only with a separate M gun
- Stud range M3 to M8
- 4-inch graphic display

CDP-99M
Power unit for capacitor discharge applications up to M10 with optional process monitoring and multi-station technology.
- Displacement measurement only with a separate M gun
- Stud range M3 to M10
- Optional Switch-4
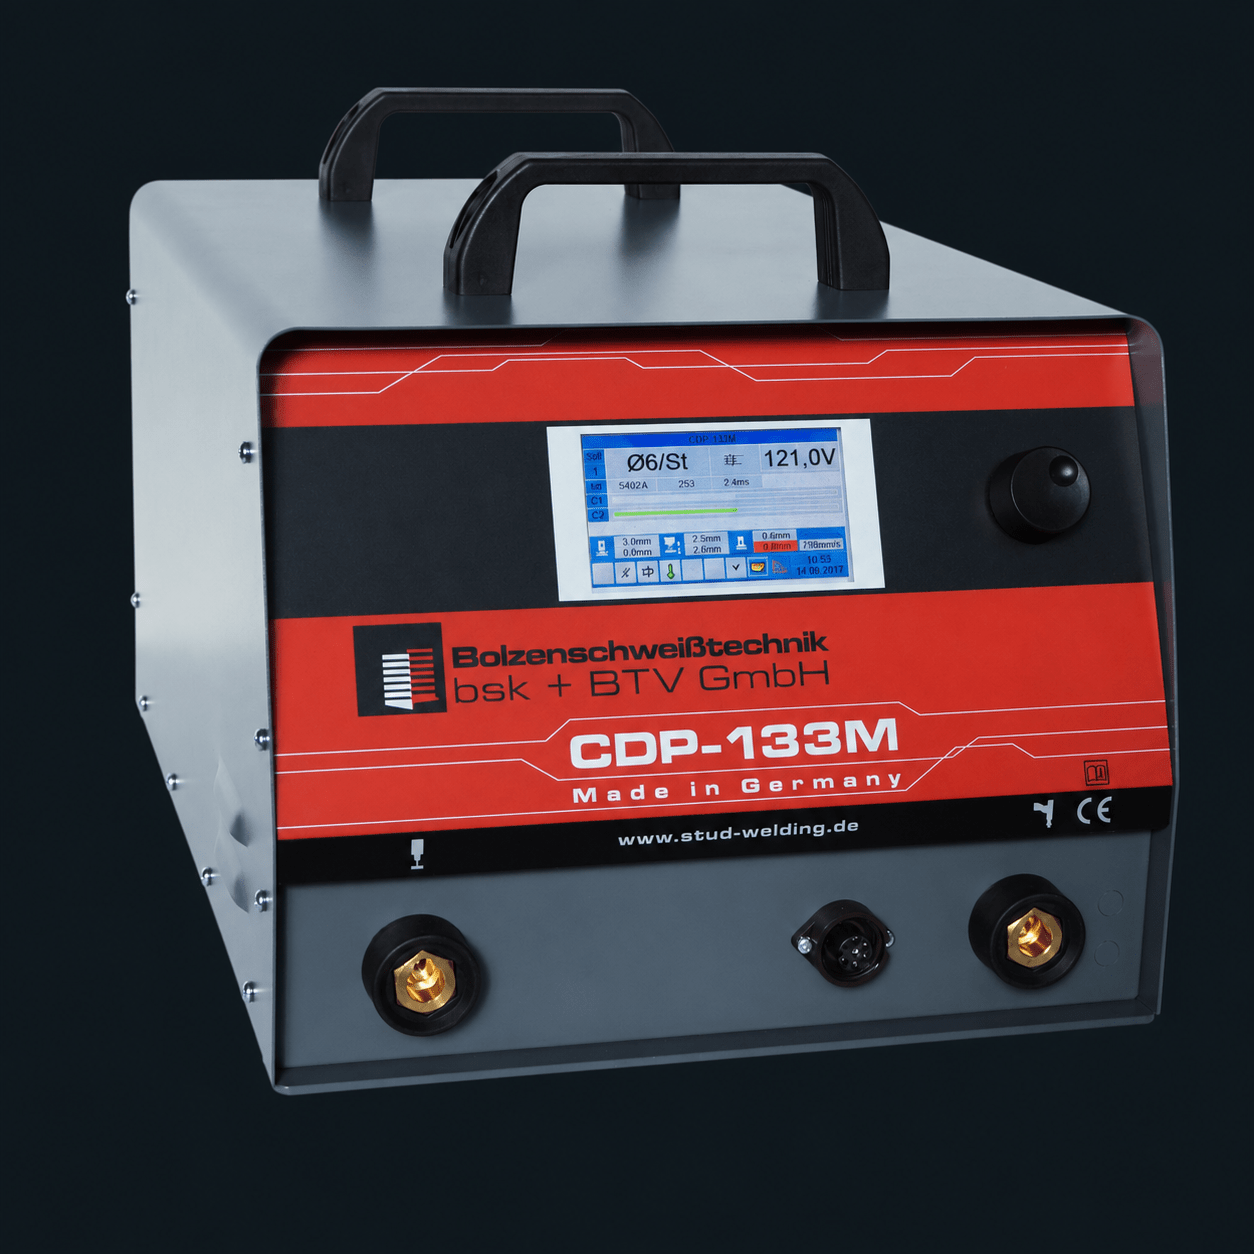
CDP-133M
High-performance CDP-M version with switchable capacitance for demanding manual and automated applications.
- Displacement measurement only with a separate M gun
- Stud range M3 to M10
- Optional process monitoring
SUITABLE MATERIALS

Select the material combination to suit the welding process
Non-heat-treatable aluminium alloys; check suitability of the material combination and process equipment

M3–M8, maximum Ø 8 mmThe usable welding range depends on the power unit, material and welding task.
COMPATIBLE WELDING ELEMENTS
The ATP-8 in detail
| Gun type | ATP-8 |
|---|---|
| Welding process | Capacitor discharge, short-cycle drawn arc and drawn arc welding |
| Applications | Unalloyed and alloyed steels and non-heat-treatable aluminium alloys; coordinate material combination and process equipment |
| Welding range | M3–M8, maximum Ø 8 mm |
| Guide | Plain bearing guide |
| Displacement measuring system | Not integrated; displacement measurement only with ATP-8M |
| Lift | 1,0–6,0 mm; continuously adjustable |
| Vertical alignment | Manual alignment without a circular spirit level |
| Plunge damping | Not fitted |
| Welding current cable | 3 m / 25 mm² |
| Housing material | Glass-fibre-reinforced thermoplastic |
| Weight without cables | 1.50 kg |
| Requirement | Automatic module in a suitable CDP-M or DAI series welder; matched stud feeding system |
Technical documents
Still unsure which option to choose?
Find the right solution for your application.
START SOLUTION FINDERFrequently asked questions
about ATP-8
Which process does ATP-8 use?
ATP-8 uses capacitor discharge, short-cycle drawn arc and drawn arc welding.
What welding range is possible?
M3–M8, maximum Ø 8 mm. The usable range depends on the power unit, material and welding task.
Which materials are intended?
Unalloyed and alloyed steels and non-heat-treatable aluminium alloys are intended. The material combination and process equipment must suit the welding task.
How is the lift adjusted?
1,0–6,0 mm. Continuously adjustable.
Does ATP-8 have integrated displacement measurement?
No. ATP-8 is the standard version without a displacement measuring system. ATP-8M also records the mechanical welding parameters.
Which power units are compatible?
CDP-66M, CDP-99M and CDP-133M, as well as DAI-1300, DAI-2300 and DAI-3300, each equipped with a suitable automatic module. The choice depends on the welding process and welding task.
For different components and welding positions
Accessories and spare parts are selected to suit the ATP-8, welding element and installation conditions. Please specify the model and version of your gun when making an enquiry.
- Accessories to suit ATP-8
- Spare parts by model and version
- Feeding components to suit the welding element

