
Automation / CNC
RAPIDOR QF
Automatic welding technology
Process different stud lengths with the same diameter: the patented length adjustment system reduces changeover effort.
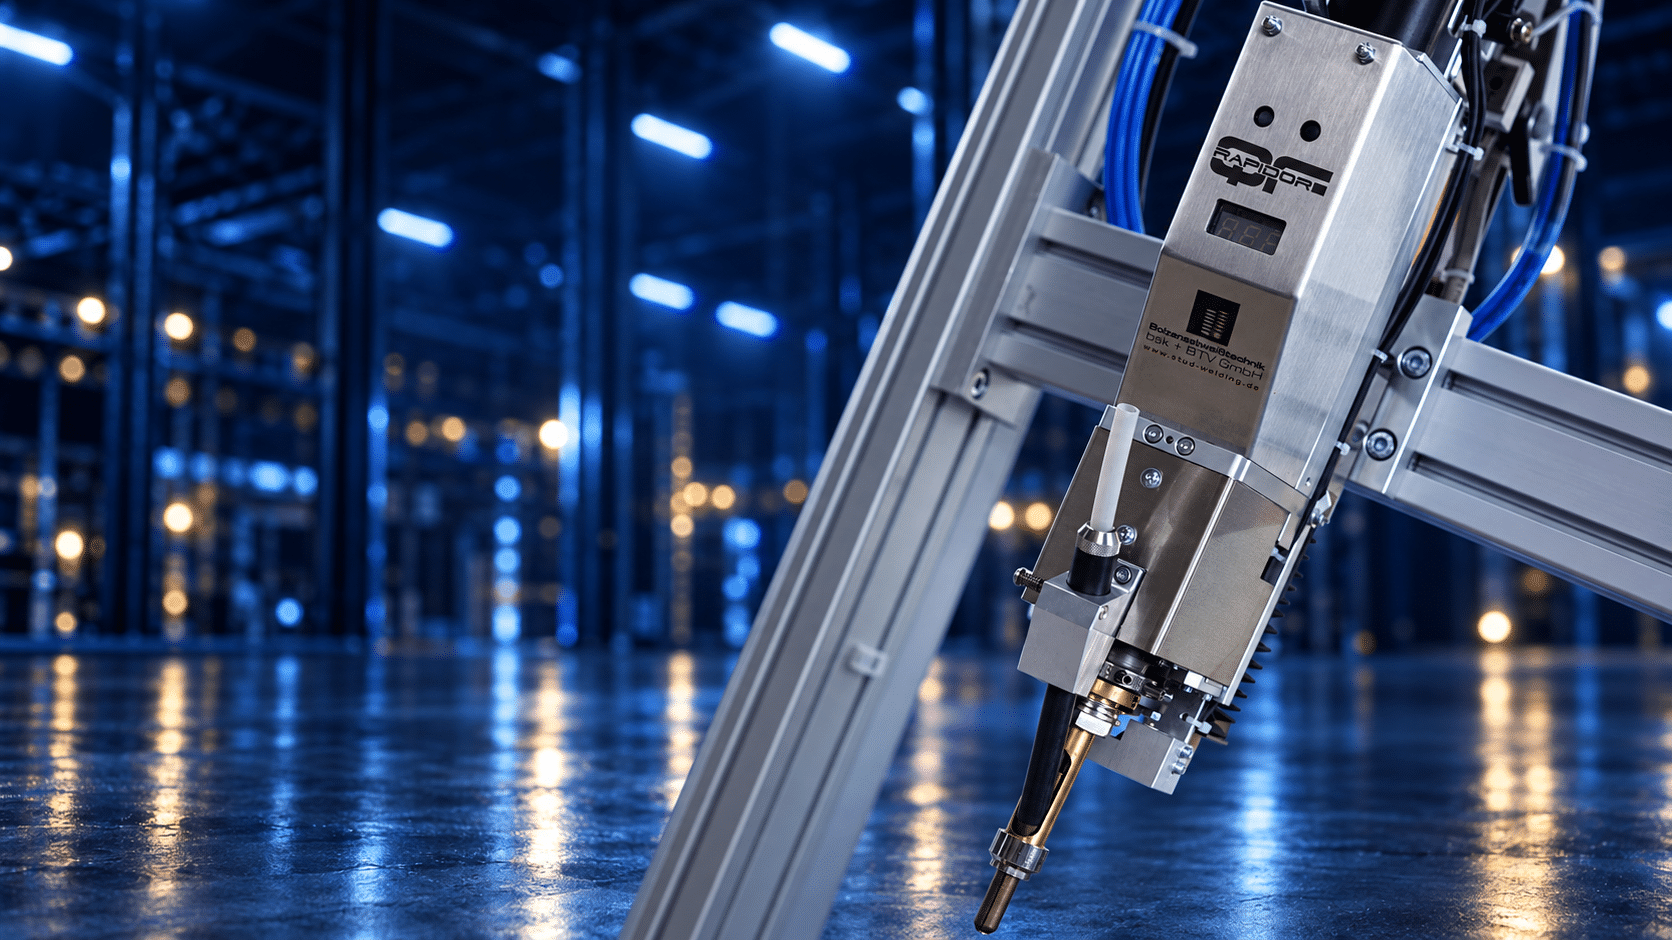
Rapidor QF automatic welding head
Rapidor QF automatic welding head
The RAPIDOR QF processes different stud lengths with the same diameter. Its patented, fully automatic stud length adjustment system covers 6–30 mm as standard.
For semi-automatic and fully automatic use with capacitor discharge, short-cycle drawn arc and drawn arc welding – for welding threaded studs, bushes and pins.
Conversion between capacitor discharge and drawn arc operation requires changing the stud holder and guide sleeve and using higher-capacity welding current cables.

Patented length adjustment
Different stud lengths.
Without time-consuming changeovers.
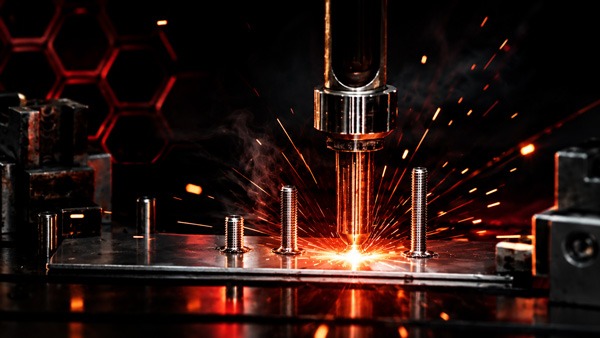
6–30 mm
One diameter. Different lengths.
The patented automatic length adjustment enables switching between different stud lengths without time-consuming mechanical changeovers.
For CNC applications, the required stud length is preselected in the relevant program block of the machine control.
At a glance
RAPIDOR QF
6–30 mm
Stud length
Ø 3–12 mm
Welding range
±0.2 mm
Positioning accuracy
up to approx. 30
studs/min¹
3,8 kg
Weight
Efficient and precise
Designed around your welding process.
Automatic length adjustment
Process different stud lengths with the same diameter fully automatically.
Preselect lengths in the program
The CNC control calls up the appropriate stud length in the relevant program block.
Precise positioning
±0.2 mm positioning accuracy. Maximum guidance in the stud holder supports precision.
Short changeover times
Fast length changes and consistent stud protrusion: no correction in the Z direction is required.
Digital display
Read lift and plunge depth directly and set up the welding head quickly.
For CNC systems
Designed for robust everyday use on CNC coordinate tables.
Suitable for semi-automatic use
Manual adjustment also enables semi-automatic operation.
Robust ball guide
The enclosed ball guide is located outside the welding area – for durability and precision.

Quick to set up.
Precisely guided.
Lift and plunge depth can be adjusted from 0–8 mm in 0.25 mm increments and read digitally.
The enclosed ball guide operates outside the welding area. Automatic stud holders and a guide sleeve allow changing to other stud diameters using proven components.
OPTIONAL
Digital stud length measuring system
Additional checks before and after welding: the optional measuring system monitors the entire stud length and checks the ignition tip length.
0,1 mm
Set tolerances
The tolerance limits before and after welding are set in 0.1 mm increments using a reference welding element.
NOK
Detect deviations
Faulty welds and lengths outside the set tolerance are detected.
STOP
Plain-text messages and program stop
The higher-level control displays errors in plain text and stops the program at the same time.
Key technical data
Technology in detail.
¹ The welding rate depends on the welding process, stud diameter and power unit.
Dimensions exclude working stroke and feed hose.
Welding range
Ø 3–12 mm
Stud lengths
6–30 mm; longer lengths on request
Positioning accuracy
±0.2 mm
Compressed air
5–7 bar, non-lubricated
Welding rate
Stud feeding up to approx. 30 studs/min¹
Dimensions (W × H × D)
65 × 440 × 90 mm
Weight
3,8 kg
Lift and plunge depth
0–8 mm in 0.25 mm increments; digital display

Data sheets and documentation
Data sheet
Spare parts catalogue
Company brochure
Custom automation
Your application.
Our technology.
Discuss your component geometry, stud types and required production process with us.

